Inverted Drum Brake Lining Hot Press
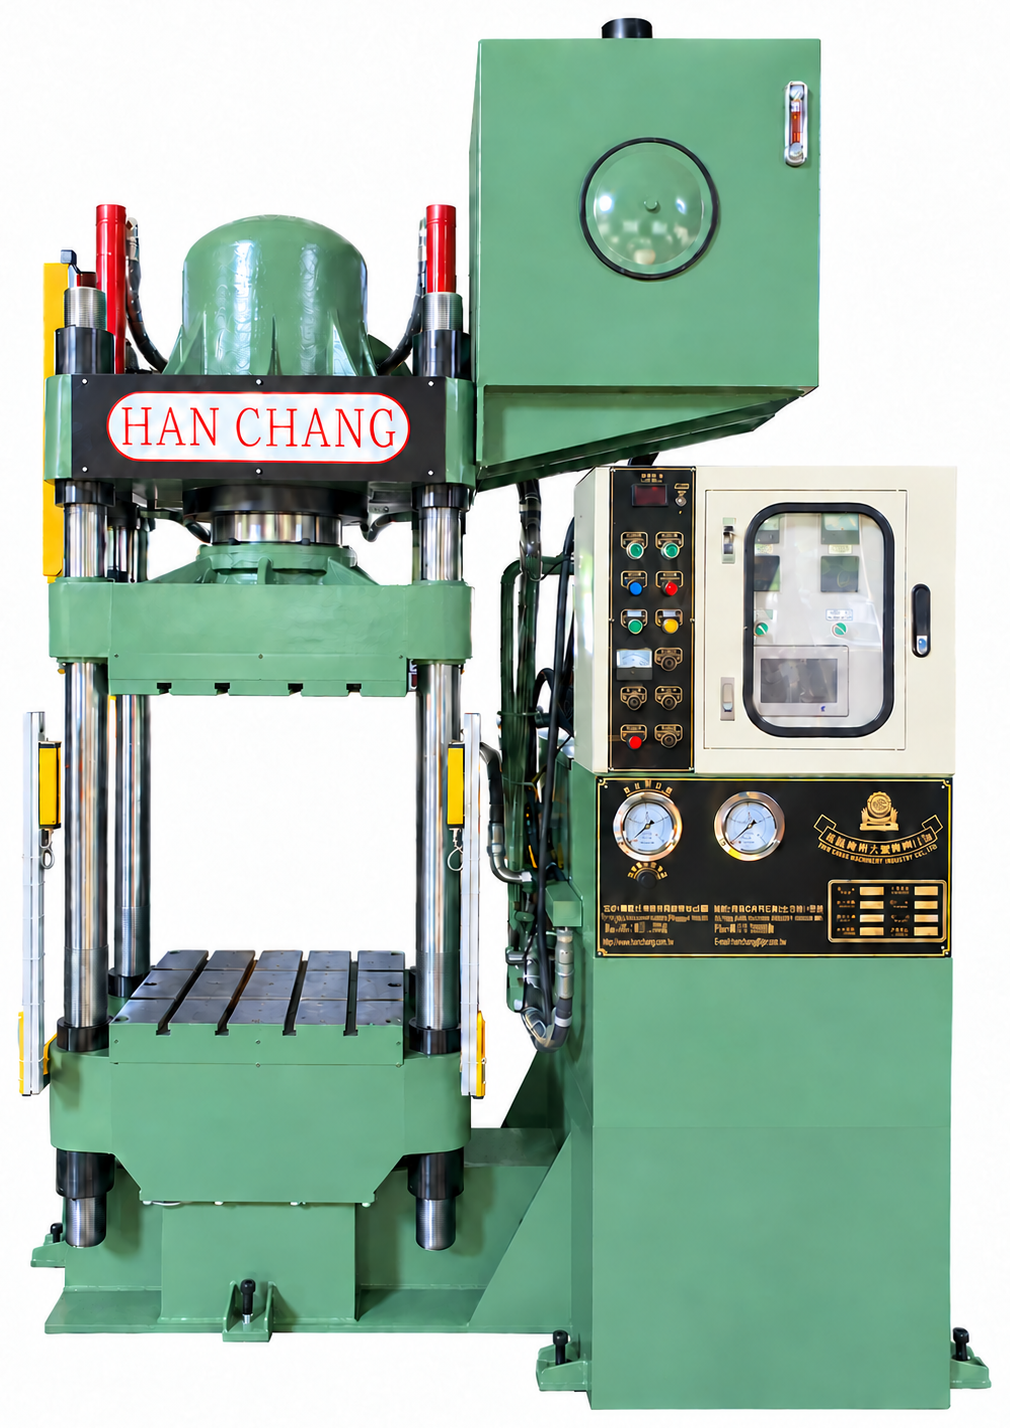
Han Chang’s Inverted Drum Brake Lining Hot Press molds and cures phenolic-bonded friction compounds into drum brake linings. A fixed lower heated platen works with hydraulic pressing from above. Customers can add their own automatic powder weighing and feeding equipment at the rear, bringing more consistent charge preparation together with reduced material-transfer and charging effort for operators.
Machine advantages
Rear material delivery can be arranged around the fixed work area, while part removal and mold cleaning take place at the front. This layout helps organize repeated charging, hot curing and removal cycles for efficient production. Han Chang supplies the hot press; the automatic weighing and feeding equipment is added by the customer and is not supplied by Han Chang.
Combine consistent charge preparation with less manual handling
Weighing compound, moving it to the press and charging it repeatedly all demand operator time and effort. Customer-installed automatic powder weighing and feeding at the rear connects measured charge preparation with material delivery. It helps prepare charges more consistently while reducing the physical workload of repeated transfer and loading, addressing two practical needs at the same workstation.
Separate incoming material from front-side operations
The stationary lower heated platen gives tooling and feeding equipment a defined point of reference. Material supply can approach from the rear, with removal and cleaning access arranged at the front. Separating these routes helps avoid crossing material and finished-part movements when planning the workstation.
Build consistent quality around the hot-curing process
Heat and hydraulic force work together to form the lining and cure its phenolic binder inside the mold. Matching temperature, molding pressure and holding time to the compound, lining thickness and tool provides a sound basis for consistent molding quality. Good charge preparation and mold care support that consistency from batch to batch.
Keep successive batches moving through a clear cycle
Sustained production depends on the complete sequence: charging, hot curing, opening, removal and mold cleaning. Rear automatic feeding helps supply material without repeated manual transfer to the work area. Coordinating that supply with the remaining operations makes the workstation easier to organize for efficient, repeated production.
Select the press around your material-supply plan
Choose the hot press for the drum lining, tooling and operating requirements. If your factory plans to add its own weighing and feeding equipment, include its footprint, rear access and delivery position in the workstation plan. This keeps press selection aligned with the equipment and handling arrangements your factory intends to use.
Drum brake lining molding process
Prepare the compound and drum lining tool
Use a phenolic-bonded friction compound suitable for hot molding and a tool designed for the lining’s curvature, length and thickness. With a customer-installed automatic weighing and feeding setup, powder is weighed before delivery for loading. The fixed lower heated platen provides the reference for the molding work area.
Charge the mold and apply heat and hydraulic force
Once the compound is in the mold, hydraulic pressing from above works with platen heating to form the material. With a customer-installed rear feeder, material delivery is coordinated with the press at the same fixed work area.
Hold under the required curing conditions
Temperature, molding pressure and holding time are matched to the compound and tool. Heat and compression form the drum lining as the phenolic-bonded material cures; resin system, section thickness and heat transfer through the mold influence the required holding period.
Open, remove the lining and prepare the next charge
After hot molding, open the tool and remove the lining using the handling arrangement suited to the mold. Operators coordinate part handling, mold cleaning and material preparation before the next molding cycle.
Drum Brake Lining Molding | Automatic Powder Weighing and Feeding
See the drum brake lining hot press working with automatic powder weighing and feeding equipment added by the customer. Rear material delivery reduces repeated carrying and charging effort and helps successive molding cycles run smoothly. The weighing and feeding equipment shown is not supplied by Han Chang.
Materials and production applications
Curved friction linings for drum brakes
The press serves the hot-molding stage of drum brake lining manufacture. Matched tooling establishes the curved profile, length and thickness while heat and hydraulic compression form and cure the friction compound. This is a focused choice for manufacturers producing the lining itself.
Phenolic-bonded friction compound molding
Phenolic-bonded friction compounds suitable for hot pressing provide the material basis for this process. Compound preparation, charge quantity, section thickness and mold heat transfer all contribute to the molding conditions. Bringing these factors together supports consistent quality across production batches.
Upgrading a manually supplied lining workstation
Factories looking to reduce repeated carrying and charging can combine a fixed hot-molding station with customer-installed rear automatic feeding. Material supply and front-side part handling can be planned separately, making this a practical route to improve workflow while retaining the operators needed for the surrounding tasks.
100–800 ton specifications and selection
Compare nine press sizes from 100 to 800 tons below. Select pressing force around the compound, total projected area and cavity count, then compare platen size, stroke and daylight. Each HCBR model has its complete specification table. Customers supply any automatic powder weighing and feeding equipment themselves.
Spec / Type HCBR-100
| Clamping force (Ton) | 100 |
|---|---|
| Plate size (m/m) | 540×605 |
| Cylinder diameter (m/m) | 265 |
| Stroke (m/m) | 460 |
| Daylight (m/m) | 690 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 5 |
| Heater capacity (Kw) | 10.6 |
| Oil reservoir capacity (gallon) | 100 |
| Machine size LxWxH (m/m) | 1940x1200x2370 |
| Net weight approx (kg) | 3700 |
Spec / Type HCBR-150
| Clamping force (Ton) | 150 |
|---|---|
| Plate size (m/m) | 660×620 |
| Cylinder diameter (m/m) | 300/315 |
| Stroke (m/m) | 480 |
| Daylight (m/m) | 700 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 7.5 |
| Heater capacity (Kw) | 10.6 |
| Oil reservoir capacity (gallon) | 100 |
| Machine size LxWxH (m/m) | 2030x1350x2370 |
| Net weight approx (kg) | 4000 |
Spec / Type HCBR-200
| Clamping force (Ton) | 200 |
|---|---|
| Plate size (m/m) | 660×620
720×720 |
| Cylinder diameter (m/m) | 368 |
| Stroke (m/m) | 500 |
| Daylight (m/m) | 820 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 10 |
| Heater capacity (Kw) | 15.2 |
| Oil reservoir capacity (gallon) | 120 |
| Machine size LxWxH (m/m) | 2300x1350x2670 |
| Net weight approx (kg) | 4500
6000 |
Spec / Type HCBR-250
| Clamping force (Ton) | 250 |
|---|---|
| Plate size (m/m) | 720×720 |
| Cylinder diameter (m/m) | 400 |
| Stroke (m/m) | 520 |
| Daylight (m/m) | 810 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 10 |
| Heater capacity (Kw) | 18.8 |
| Oil reservoir capacity (gallon) | 150 |
| Machine size LxWxH (m/m) | 2410x1350x2780 |
| Net weight approx (kg) | 6800 |
Spec / Type HCBR-300
| Clamping force (Ton) | 300 |
|---|---|
| Plate size (m/m) | 630×630
720×720 900×860 |
| Cylinder diameter (m/m) | 450 |
| Stroke (m/m) | 560 |
| Daylight (m/m) | 810 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 15 |
| Heater capacity (Kw) | 20 |
| Oil reservoir capacity (gallon) | 200 |
| Machine size LxWxH (m/m) | 2480x1490x2945 |
| Net weight approx (kg) | 6500
7500 9500 |
Spec / Type HCBR-400
| Clamping force (Ton) | 400 |
|---|---|
| Plate size (m/m) | 630×630 |
| Cylinder diameter (m/m) | 500 |
| Stroke (m/m) | 560 |
| Daylight (m/m) | 950 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 15 |
| Heater capacity (Kw) | 27 |
| Oil reservoir capacity (gallon) | 250 |
| Machine size LxWxH (m/m) | 2580x1500x3800 |
| Net weight approx (kg) | 6800
8000 10000 |
Spec / Type HCBR-500
| Clamping force (Ton) | 500 |
|---|---|
| Plate size (m/m) | 800×800
900×900 |
| Cylinder diameter (m/m) | 560 |
| Stroke (m/m) | 580 |
| Daylight (m/m) | 1000 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 15 |
| Heater capacity (Kw) | 30 |
| Oil reservoir capacity (gallon) | 250 |
| Machine size LxWxH (m/m) | 2810x1705x3135 |
| Net weight approx (kg) | 10000
13500 |
Spec / Type HCBR-600
| Clamping force (Ton) | 600 |
|---|---|
| Plate size (m/m) | 1000×1000 |
| Cylinder diameter (m/m) | 620 |
| Stroke (m/m) | 610 |
| Daylight (m/m) | 1020 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 20 |
| Heater capacity (Kw) | 30 |
| Oil reservoir capacity (gallon) | 300 |
| Machine size LxWxH (m/m) | 3000x1750x4100 |
| Net weight approx (kg) | 14000
16500 |
Spec / Type HCBR-800
| Clamping force (Ton) | 800 |
|---|---|
| Plate size (m/m) | 1800×1400 |
| Cylinder diameter (m/m) | 700 |
| Stroke (m/m) | 700 |
| Daylight (m/m) | 1060 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 30 |
| Heater capacity (Kw) | 40 |
| Oil reservoir capacity (gallon) | 355 |
| Machine size LxWxH (m/m) | 3220x1850x4350 |
| Net weight approx (kg) | 26000 |
Consider tool mounting, mold height, release clearance, rear feeding space, front-side removal and cleaning access, and guarding. Where customers add their own weighing and feeding equipment, include its space and operating requirements in the layout. Han Chang quotes the agreed hot-press scope, excluding customer-supplied weighing and feeding equipment.
Feeding equipment and workstation layout
Send a lining photo, drawing or approximate dimensions to begin the discussion. Han Chang can work through compound requirements, cavity count and planned output with you, then compare pressing force, platen space, stroke and daylight for the job.
Send drawings of any customer-sourced feeding equipment, together with photos of the current charging method and available space. These help Han Chang discuss press dimensions and working access. Automatic weighing and feeding equipment remains customer-supplied and is not included in Han Chang’s equipment supply.
Buyer questions
What does an inverted drum brake lining hot press make?
An inverted drum brake lining hot press forms phenolic-bonded friction compound into molded linings for drum brakes. Han Chang’s design uses a fixed lower heated platen and hydraulic pressing from above to apply heat and force inside the mold. The lining’s curvature and dimensions are established by the product tooling.
What can customer-installed automatic powder weighing and feeding improve?
The customer-installed rear system combines powder weighing with material delivery for loading. It helps prepare measured charges more consistently and reduces the effort of repeated manual transfer and charging. Feeding is arranged around the fixed lower work area, while front-side access can serve part handling and mold cleaning.
Why choose a fixed lower heated platen?
A fixed lower heated platen gives the mold, material delivery and part-collection positions a stationary reference during pressing. Hydraulic force is applied from above. This arrangement is useful when planning a drum lining workstation with rear feeding and front-side operating access.
What supports consistent quality in hot-molded drum linings?
Consistent drum lining molding depends on the friction formulation, charge quantity, mold condition, temperature, molding pressure and holding time. Heat and hydraulic compression shape and cure the phenolic-bonded material. Matching those conditions to the lining and maintaining consistent material preparation and mold cleaning supports repeatable batch quality.
How is sustained production organized, and what determines output?
Production runs through repeated charging, hot curing, opening, part removal and mold-cleaning cycles. A customer-installed rear feeder supplies material while operators coordinate the surrounding tasks. Output depends on cavity count, curing time and the time needed for loading, removal and mold preparation, so the complete cycle is considered when discussing a production target.
How does a lining hot press differ from a brake shoe bonding or riveting machine?
A drum brake lining hot press molds and cures friction compound into a lining. Brake shoe bonding and riveting machines attach a lining to a shoe body as an assembly operation. Choose hot-molding equipment when the requirement is to manufacture the friction lining; plan shoe assembly equipment separately for the intended product design.
Does Han Chang supply the automatic weighing and feeding equipment?
No. Han Chang supplies the drum brake lining hot press. The automatic weighing and feeding equipment shown in the video was added by the customer. Share drawings of your own equipment and the available space to discuss press selection and working access; compatibility with every third-party feeder is not assumed.
What information is needed to select a model and request a quote?
Begin with a drum lining photo or drawing, dimensions and planned output. If tooling already exists, include its footprint, height and cavity count. Han Chang can discuss pressing force against the compound’s molding requirements and total projected area, then match platen size, stroke and daylight. HCBR is the specification and quotation reference; rear automatic feeding can be included in the configuration discussion.
Take repetitive material handling out of your next press upgrade
Send Han Chang your drum lining drawing, existing tool details or a photo of the current charging operation. Discuss the appropriate inverted hot press and request a quotation. If you have your own feeding equipment, include its drawings so press selection can take the intended workstation layout into account.