
Brake Pad Hot Press Molding Machine | Internal Mold-Support Type
Han Chang’s internal mold-support brake pad hot press combines heat and hydraulic force to mold and cure phenolic-bonded friction compounds for disc brake pads, drum brake linings and vehicle friction parts.
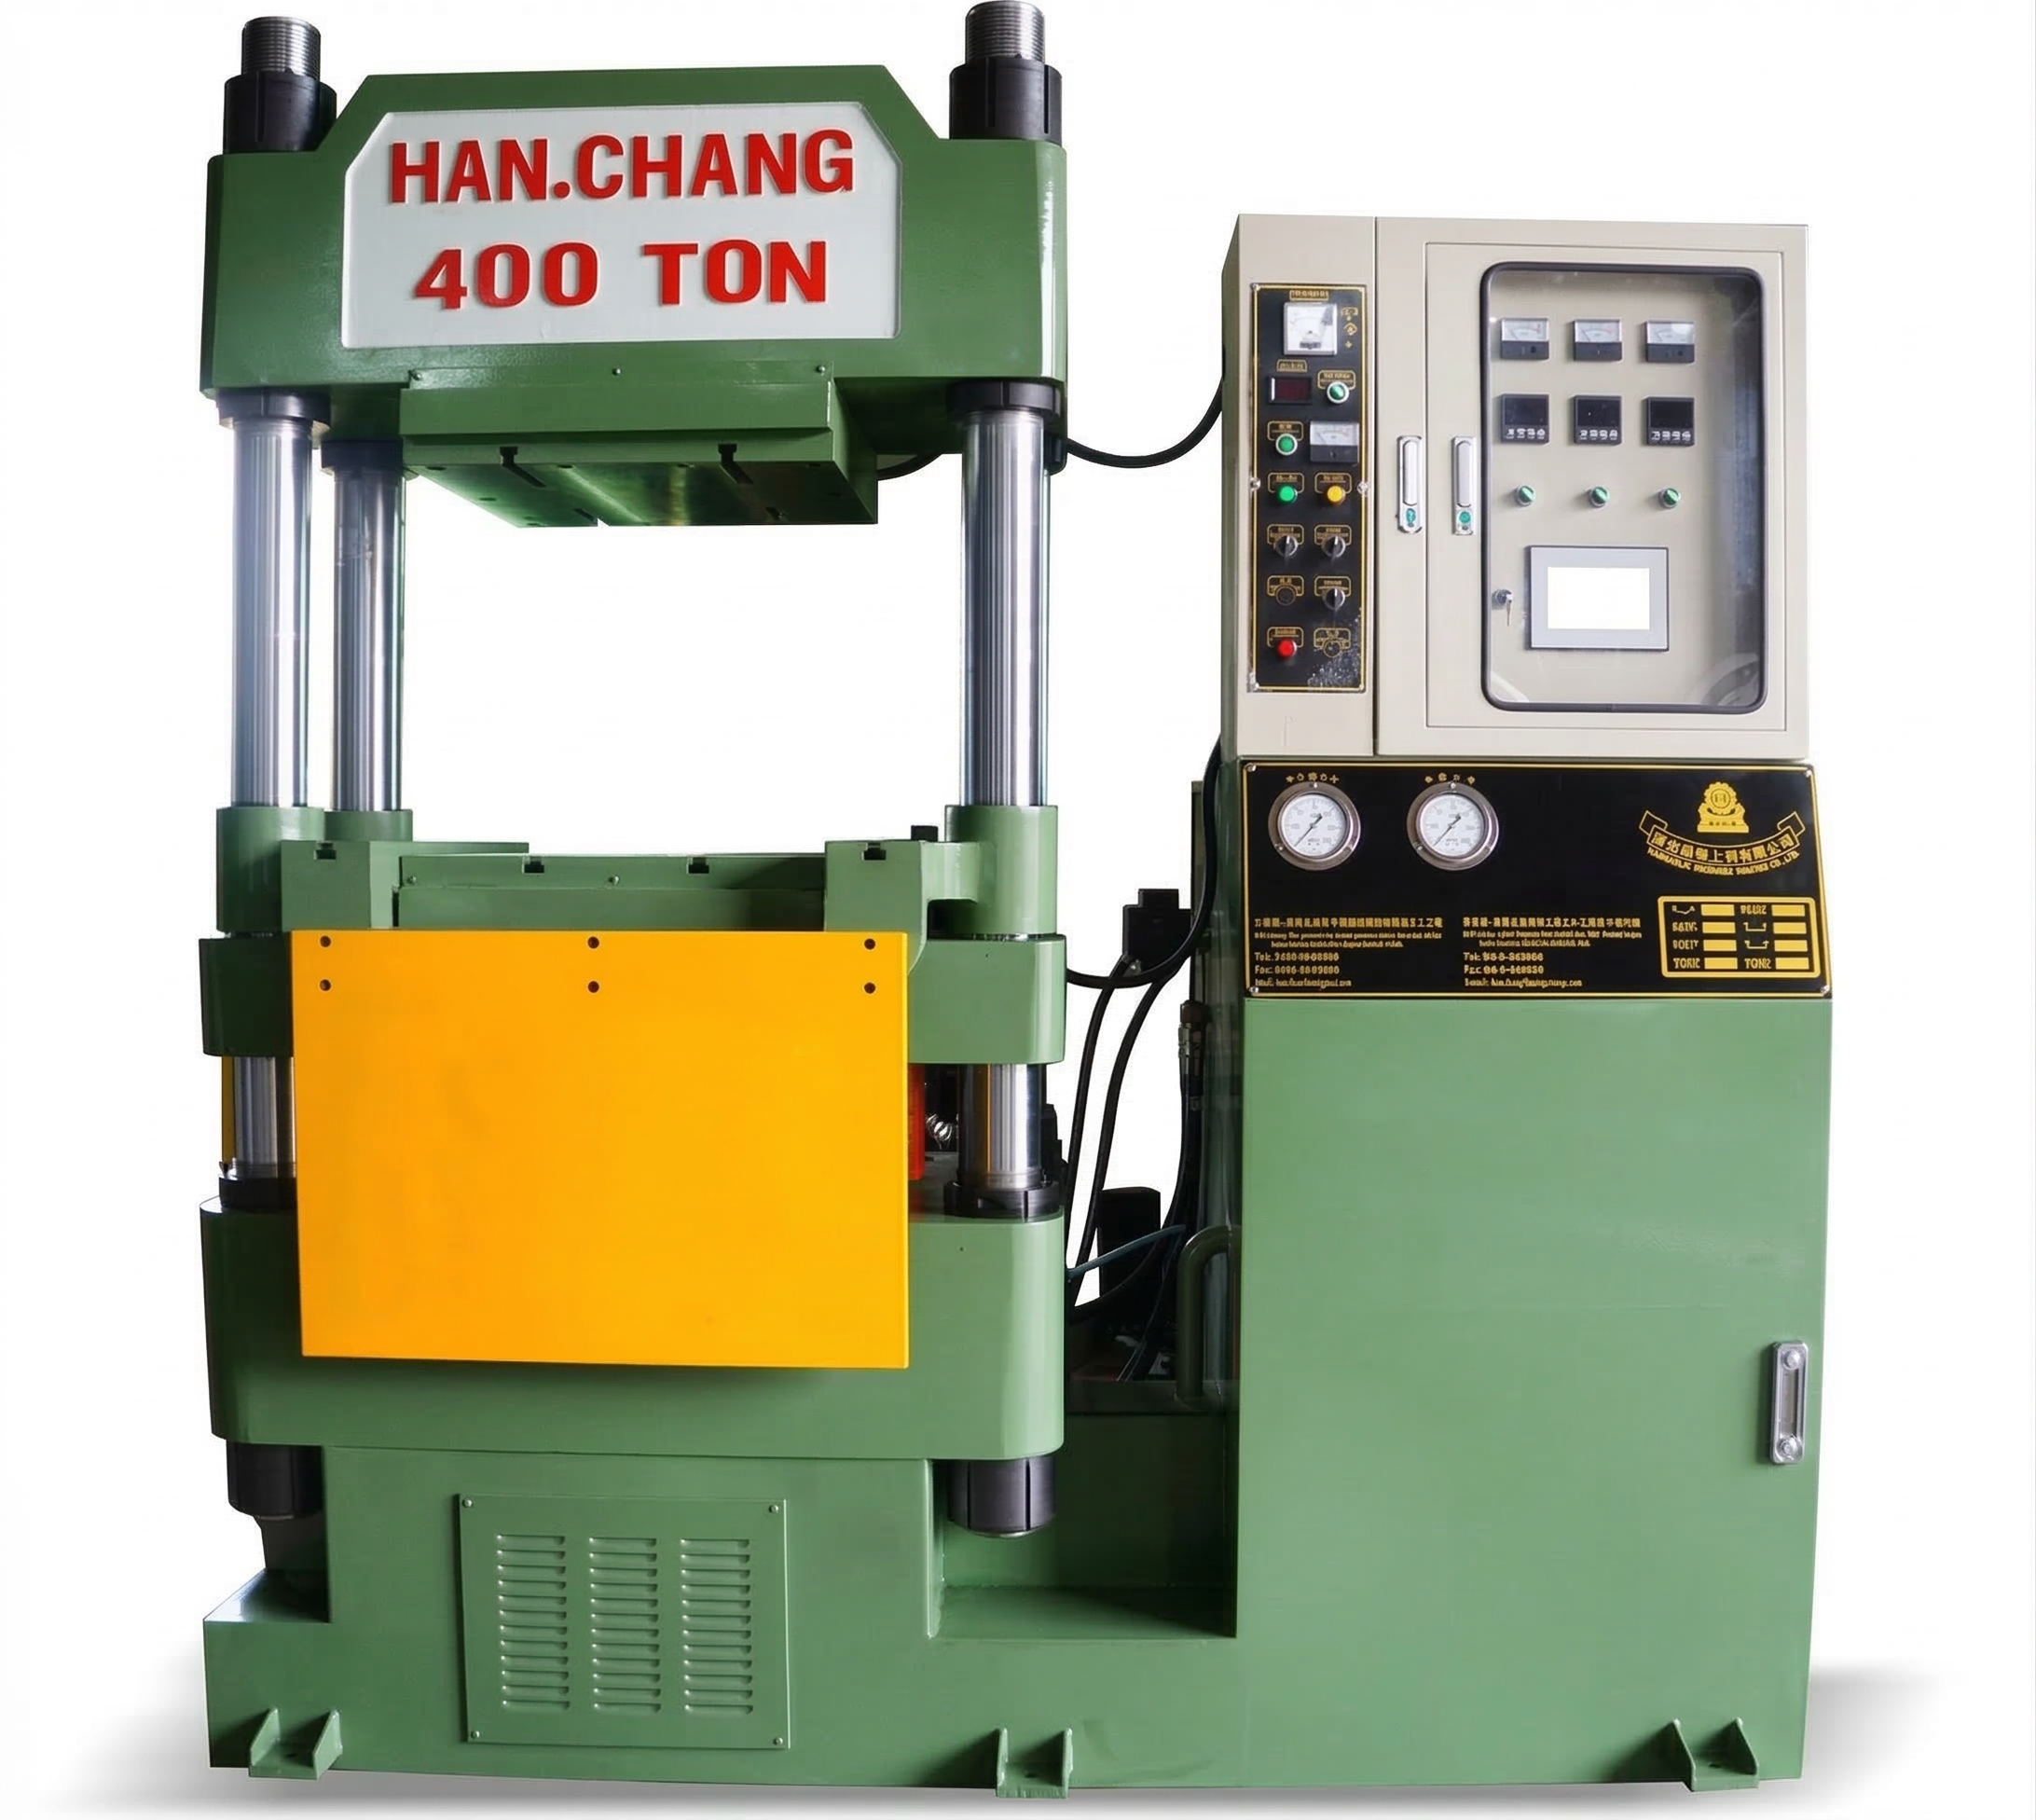
Machine advantages
Choose this machine as a practical starting point for a tooling-led brake manufacturing workstation. It shares all operating motions with the large-format internal mold-support press in a smaller physical size, so the equipment choice can follow your molds and factory layout.
Combine heat and pressure for friction-material molding
Heat and hydraulic force compact the friction compound to the tool shape and cure its phenolic binder system. This is a core production stage for disc brake pads and molded drum linings. With the appropriate formulation, charge and holding conditions, the press supports consistent batch molding and prepares parts for downstream processing.
Build disc-pad and drum-lining production around the tooling
The press serves disc brake pads, drum brake linings and vehicle friction moldings. Tooling establishes product geometry and cavity layout; backing plates are incorporated where the product and mold design require them. Start the equipment specification with the parts you intend to manufacture.
Keep the operating method while choosing the machine size
This machine and the large-format press share the same mold-support, opening, demolding and operating motions. Where the products and molds suit the smaller machine, use that physical scale to plan the workstation and handling arrangements.
Plan mold installation and daily handling together
Consider mold support, fastening, opening access, part removal and mold transport as one workstation. Matching both the molding load and working space helps connect the press with existing operators and material-handling routes.
Molding process
Prepare the compound and tooling
Prepare the friction compound to the product formulation and load it according to the tooling design. For disc pads with steel backing plates, include the appropriate backing-plate preparation and bonding system.
Apply heat and hydraulic force
Heat and compress the material in the mold. Select temperature and molding pressure around the actual formulation, projected area under load and tooling requirements.
Hold for curing
Maintain the holding and curing conditions required by the resin system, part thickness and mold heat transfer, managing the compound and hot-molding conditions together.
Open and remove the parts
After molding, follow the machine and tooling’s opening, demolding and removal arrangement. Unload the parts and prepare the mold for the next production cycle.
Materials and production applications
Disc brake pads
Manufacture friction blocks for automotive disc brake systems by hot-compression molding phenolic-bonded compounds. The mold establishes the pad outline and cavity layout; for steel-backed pads, it also accommodates the specified relationship between the friction charge and backing plate. An internal mold-support hot press provides this molding stage for a tooling-led production cell, helping factories organize batches around their brake-pad designs. Backing-plate surface preparation and bonding remain part of the product process.
Drum brake linings and vehicle friction parts
Drum brake linings are curved friction components that work against the brake drum, with applications in passenger cars, light trucks and trucks. Heated tooling forms and cures the compound to the required lining profile for subsequent processing and assembly. Use this press to build a hot-molding workstation around suitable existing lining molds, matching machine size and tooling access with the way operators remove parts and change tools.
Ceramic, semi-metallic and non-asbestos compounds
Ceramic, semi-metallic and non-asbestos brake products can use phenolic-bonded formulations suited to hot pressing. The binder holds fibers, fillers and friction-modifying ingredients together as heat and pressure form the molded part. Han Chang can match heating and molding-load requirements to the actual compound and tool, providing a hydraulic hot molding press for the intended friction-material process.
Specifications and selection
Displayed configuration: 400 tons of press force and a 630×630 mm platen. The HCBR tables provide range comparisons; the agreed machine quotation defines the equipment supplied.
Spec / Type HCBR-100
| Clamping force (Ton) | 100 |
|---|---|
| Plate size (m/m) | 540×605 |
| Cylinder diameter (m/m) | 265 |
| Stroke (m/m) | 460 |
| Daylight (m/m) | 690 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 5 |
| Heater capacity (Kw) | 10.6 |
| Oil reservoir capacity (gallon) | 100 |
| Machine size LxWxH (m/m) | 1940x1200x2370 |
| Net weight approx (kg) | 3700 |
Spec / Type HCBR-150
| Clamping force (Ton) | 150 |
|---|---|
| Plate size (m/m) | 660×620 |
| Cylinder diameter (m/m) | 300/315 |
| Stroke (m/m) | 480 |
| Daylight (m/m) | 700 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 7.5 |
| Heater capacity (Kw) | 10.6 |
| Oil reservoir capacity (gallon) | 100 |
| Machine size LxWxH (m/m) | 2030x1350x2370 |
| Net weight approx (kg) | 4000 |
Spec / Type HCBR-200
| Clamping force (Ton) | 200 |
|---|---|
| Plate size (m/m) | 660×620
720×720 |
| Cylinder diameter (m/m) | 368 |
| Stroke (m/m) | 500 |
| Daylight (m/m) | 820 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 10 |
| Heater capacity (Kw) | 15.2 |
| Oil reservoir capacity (gallon) | 120 |
| Machine size LxWxH (m/m) | 2300x1350x2670 |
| Net weight approx (kg) | 4500
6000 |
Spec / Type HCBR-250
| Clamping force (Ton) | 250 |
|---|---|
| Plate size (m/m) | 720×720 |
| Cylinder diameter (m/m) | 400 |
| Stroke (m/m) | 520 |
| Daylight (m/m) | 810 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 10 |
| Heater capacity (Kw) | 18.8 |
| Oil reservoir capacity (gallon) | 150 |
| Machine size LxWxH (m/m) | 2410x1350x2780 |
| Net weight approx (kg) | 6800 |
Spec / Type HCBR-300
| Clamping force (Ton) | 300 |
|---|---|
| Plate size (m/m) | 630×630
720×720 900×860 |
| Cylinder diameter (m/m) | 450 |
| Stroke (m/m) | 560 |
| Daylight (m/m) | 810 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 15 |
| Heater capacity (Kw) | 20 |
| Oil reservoir capacity (gallon) | 200 |
| Machine size LxWxH (m/m) | 2480x1490x2945 |
| Net weight approx (kg) | 6500
7500 9500 |
Spec / Type HCBR-400
| Clamping force (Ton) | 400 |
|---|---|
| Plate size (m/m) | 630×630 |
| Cylinder diameter (m/m) | 500 |
| Stroke (m/m) | 560 |
| Daylight (m/m) | 950 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 15 |
| Heater capacity (Kw) | 27 |
| Oil reservoir capacity (gallon) | 250 |
| Machine size LxWxH (m/m) | 2580x1500x3800 |
| Net weight approx (kg) | 6800
8000 10000 |
Spec / Type HCBR-500
| Clamping force (Ton) | 500 |
|---|---|
| Plate size (m/m) | 800×800
900×900 |
| Cylinder diameter (m/m) | 560 |
| Stroke (m/m) | 580 |
| Daylight (m/m) | 1000 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 15 |
| Heater capacity (Kw) | 30 |
| Oil reservoir capacity (gallon) | 250 |
| Machine size LxWxH (m/m) | 2810x1705x3135 |
| Net weight approx (kg) | 10000
13500 |
Spec / Type HCBR-600
| Clamping force (Ton) | 600 |
|---|---|
| Plate size (m/m) | 1000×1000 |
| Cylinder diameter (m/m) | 620 |
| Stroke (m/m) | 610 |
| Daylight (m/m) | 1020 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 20 |
| Heater capacity (Kw) | 30 |
| Oil reservoir capacity (gallon) | 300 |
| Machine size LxWxH (m/m) | 3000x1750x4100 |
| Net weight approx (kg) | 14000
16500 |
Spec / Type HCBR-800
| Clamping force (Ton) | 800 |
|---|---|
| Plate size (m/m) | 1800×1400 |
| Cylinder diameter (m/m) | 700 |
| Stroke (m/m) | 700 |
| Daylight (m/m) | 1060 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 30 |
| Heater capacity (Kw) | 40 |
| Oil reservoir capacity (gallon) | 355 |
| Machine size LxWxH (m/m) | 3220x1850x4350 |
| Net weight approx (kg) | 26000 |
Mold footprint, height, support and fastening define installation space. Material molding pressure, total projected area under load and tooling loads define force requirements. Match daylight, stroke and heating to mold height, part removal and curing needs. Product photos or drawings are enough to start; you do not need to calculate the tonnage first.
Equipment integration and technical discussion
Han Chang manufactures hydraulic hot molding equipment and can discuss the press using your product drawings, existing molds and workstation photos. Include mold weight, support, fastening, material staging and part collection to connect the equipment with daily factory work. For a brake pad production line, Han Chang also offers one-stop services, with the press and companion equipment identified in the quotation.
Compare the press, tooling interfaces, heating, loading and unloading, mold transport, guarding and site power requirements on equal scope. Then plan output around parts per mold load and the time for curing, cleaning and handling.
Buyer questions
How do I choose between the internal mold-support press and the large-format machine?
Both use the same mold-support, opening, demolding and operating motions; their physical size differs. Choose this machine where the products and tooling suit the smaller build, and compare the large-format press when the workstation calls for a larger configuration. Mold dimensions, installation and part-removal space, and molding load guide the choice.
How should I use the specifications shown on this page?
The displayed configuration has 400 tons of press force and a 630×630 mm platen for comparison with tooling dimensions and molding loads. The range tables help compare specifications. Han Chang identifies the force, platen and other equipment supplied in the machine quotation so that purchasing decisions use a common scope.
Which brake products and friction materials is it intended for?
Applications include disc brake pads, drum brake linings and friction parts for passenger cars, light trucks and trucks. Ceramic, semi-metallic and non-asbestos compounds can be considered when they use a phenolic-bonded formulation suitable for hot pressing. Select the process conditions around the actual compound and tooling.
When should I compare the large-format internal mold-support hot press?
Compare the large-format machine when you need a larger physical configuration, more tooling installation space or a different handling arrangement. Both machines share the same operating motions. Match the complete tooling, molding loads and workstation first, then plan output from cavity count and the full curing and handling cycle.
How do existing molds and handling methods affect the configuration?
Mold dimensions, height, weight and fastening guide the installation and part-removal requirements. Photos of the current workstation show how material arrives, where parts are collected and how molds are changed. Together, these inputs help plan tooling access, handling routes and guarding around the press.
Can I request a quote without a complete machine specification?
Yes. Send the product photos, dimensions, compound information or equipment details already available. Add mold drawings and cavity counts if you have them. Han Chang can begin discussing an internal mold-support hot press from that starting point.
How should we compare machine prices and output?
Use the same tooling, molding loads, heating and handling requirements when comparing quotations, and identify the press and companion equipment in the supply scope. Plan output from parts per mold load and the complete cycle, including curing, cleaning and part removal, so the investment reflects actual factory work.
Discuss an internal mold-support hot press for your brake products
Send Han Chang the product photos, dimensions, compound information or existing equipment details you already have. Mold drawings and workstation photos can follow as the discussion develops; a complete technical specification is not required to start an inquiry.
Related technical information
- Brake pad hot press equipment FAQ
- Friction material hot press planning
- Brake pad machine tonnage from 100T to 800T
- Brake pad molding defects and yield
Brake Pad Hot Press Molding Machine | Automated Production by Han Chang
Taiwan Hydraulic Compression Molding Machine Manufacturer | Han Chang Machinery
Compression Molding Machine Parts Explained | Han Chang #Shorts




