Multi-Station Brake Pad Molding Machine
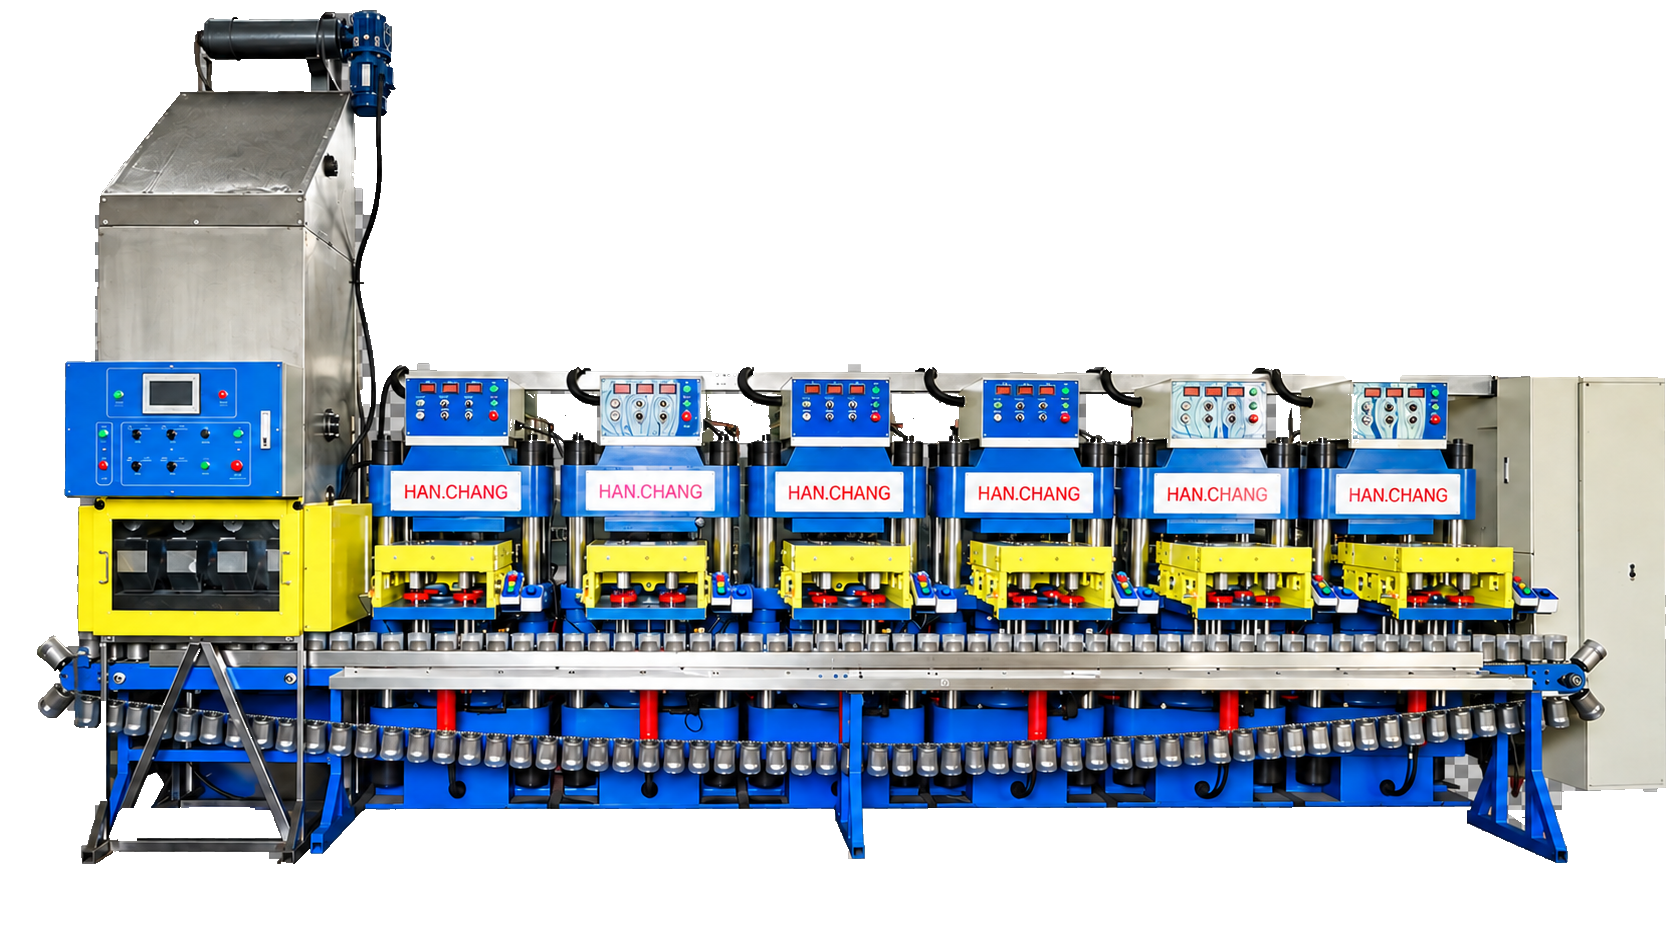
Han Chang’s Multi-Station Brake Pad Molding Machine uses six closely spaced workstations to hot-compression mold phenolic-bonded friction compounds into disc brake pads. The close station layout supports one-operator tending with less walking.
Machine advantages
Choose this six-station brake pad hot press when your factory needs to produce several pad designs and make better use of operator time. Organize work around the products and tooling, keep neighboring stations within a short working route, and improve day-to-day efficiency. Appropriate charging and curing conditions support consistent quality across production batches.
Spend less time walking between presses
Six closely spaced stations help one operator move between loading, molding and part-removal tasks along a shorter working route. Keeping these tasks at neighboring stations reduces walking between widely separated machines and makes day-to-day tending more efficient.
Organize production around several pad designs
Use the six-station arrangement to schedule hot-molding work for multiple brake pad products and their molds. It is a practical choice for manufacturers handling a varied product mix who want to keep station work together and easier to oversee.
Form and cure for consistent molding quality
Heat and hydraulic force compact the friction compound to the mold shape and cure its phenolic binder. Match the charge and holding conditions to the material to support consistent brake pad molding from batch to batch.
Select capacity at the station level
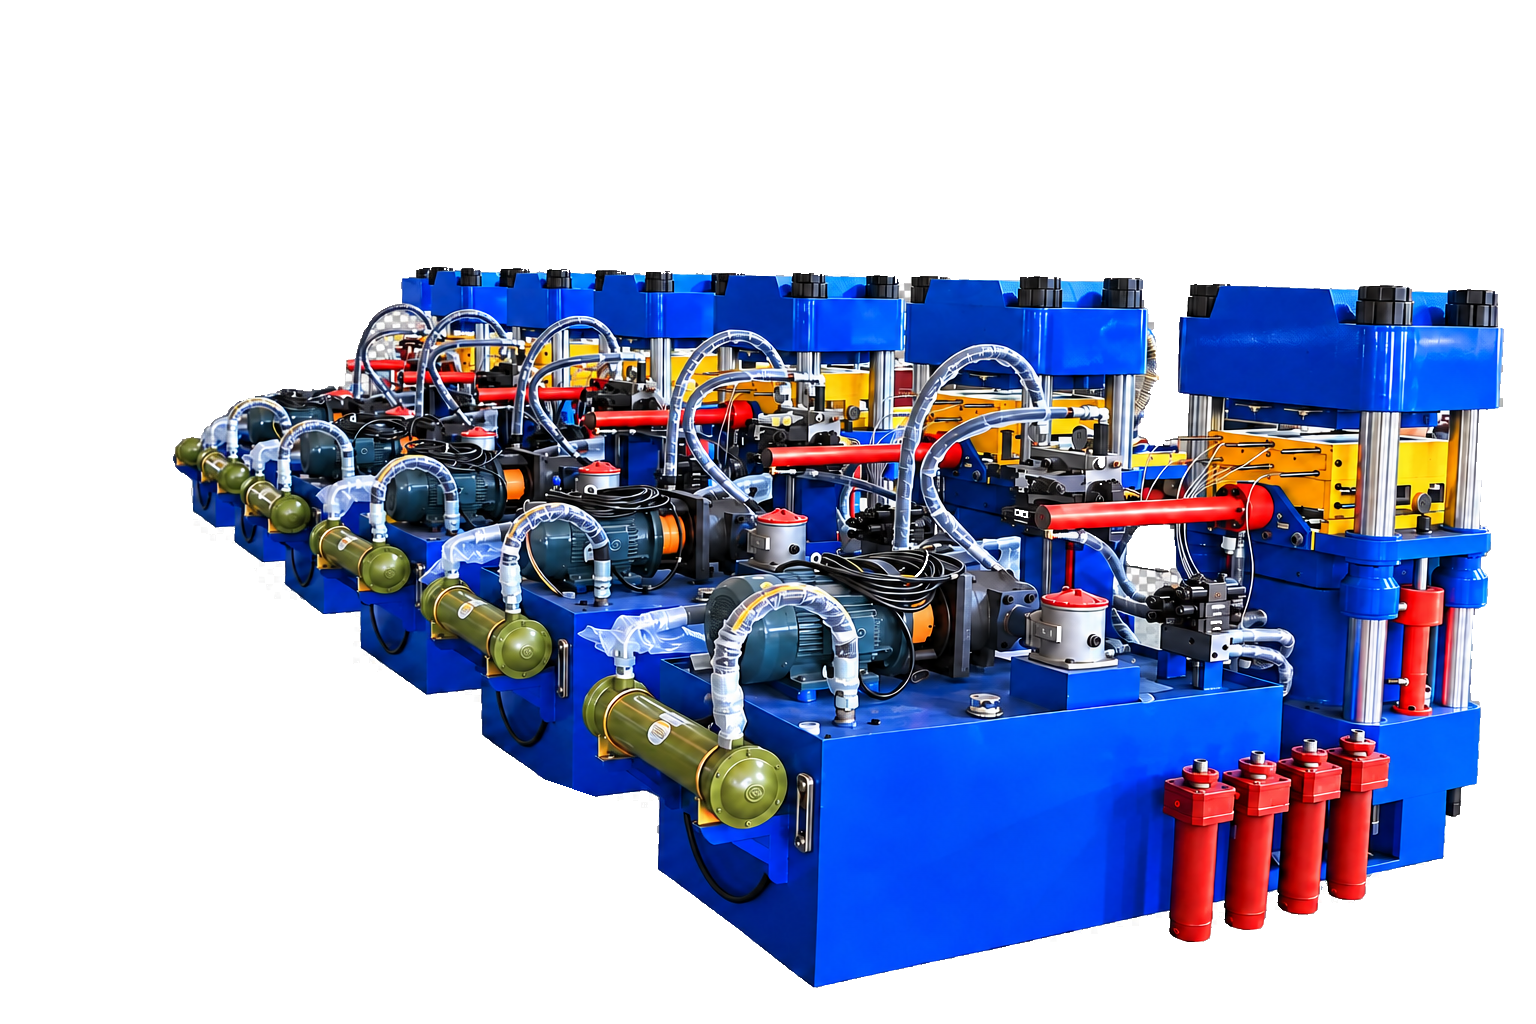
All five models provide six stations, so compare the molding load required at each station before choosing a model. Platen dimensions, cavity layout, daylight and stroke then help match the press to the complete tool and its working space.
Hot pressing and machine video
Prepare the charge and load the mold
Prepare the friction compound to the pad formulation and load the required charge according to the tool design. For steel-backed pads, include the specified backing-plate preparation, bonding system and placement.
Apply heat and hydraulic compression
Heat and compress the compound in the mold to form the brake pad profile. Molding temperature and pressure are matched to the actual formulation, projected area under load and tooling requirements.
Hold for in-mold curing
Maintain the hot-pressing and holding conditions needed to cure the phenolic binder system. Resin chemistry, pad thickness and heat transfer through the mold guide this stage and support consistent batch quality.
Open, remove and prepare the next charge
Open the mold after forming and remove the parts using the tooling’s release and handling arrangement. Clean and prepare the mold for the next charge. Neighboring stations keep these operator tasks along a short route between presses.

Materials and production applications
Automotive disc brake pads
Hot-compression mold friction blocks for automotive disc brake systems. The tooling defines pad outline, thickness and cavity layout; six neighboring stations provide a practical arrangement for producing multiple pad designs and organizing batch work around the operator.
Steel-backed brake pads
Where the product and tooling require a steel backing plate, arrange the plate and friction charge together for hot molding. The specified surface preparation and bonding system accompany the molding process, preparing the parts for subsequent finishing and assembly.
Ceramic, semi-metallic and non-asbestos formulations
These brake pad types can use phenolic-bonded friction compounds suitable for hot pressing. Heat and pressure bring the binder, fibers, fillers and friction-modifying ingredients together into a molded part. Match the molding conditions to the actual compound and tool for the intended pad product.
Per-station specifications and model selection
Choose from five models rated at 150, 200, 250, 300 or 400 tons per station; every model has six workstations. All values in the tables are per-station specifications, including dimensions, weight, motor rating and heater capacity. Dimensions, weight and total electrical requirements for the complete six-station installation are supplied separately for the agreed configuration.
HCBR-150T6S · Per-station specifications
| Clamping force (Ton) | 150 |
|---|---|
| Plate size (m/m) | 660×620 |
| Cylinder diameter (m/m) | 300/315 |
| Stroke (m/m) | 480 |
| Daylight (m/m) | 700 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 7.5 |
| Heater capacity (Kw) | 10.6 |
| Oil reservoir capacity (gallon) | 100 |
| Machine size LxWxH (m/m) | 2030x1350x2370 |
| Net weight approx (kg) | 4000 |
HCBR-200T6S · Per-station specifications
| Clamping force (Ton) | 200 |
|---|---|
| Plate size (m/m) | 660×620
720×720 |
| Cylinder diameter (m/m) | 368 |
| Stroke (m/m) | 500 |
| Daylight (m/m) | 820 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 10 |
| Heater capacity (Kw) | 15.2 |
| Oil reservoir capacity (gallon) | 120 |
| Machine size LxWxH (m/m) | 2300x1350x2670 |
| Net weight approx (kg) | 4500
6000 |
HCBR-250T6S · Per-station specifications
| Clamping force (Ton) | 250 |
|---|---|
| Plate size (m/m) | 720×720 |
| Cylinder diameter (m/m) | 400 |
| Stroke (m/m) | 520 |
| Daylight (m/m) | 810 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 10 |
| Heater capacity (Kw) | 18.8 |
| Oil reservoir capacity (gallon) | 150 |
| Machine size LxWxH (m/m) | 2410x1350x2780 |
| Net weight approx (kg) | 6800 |
HCBR-300T6S · Per-station specifications
| Clamping force (Ton) | 300 |
|---|---|
| Plate size (m/m) | 630×630
720×720 900×860 |
| Cylinder diameter (m/m) | 450 |
| Stroke (m/m) | 560 |
| Daylight (m/m) | 810 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 15 |
| Heater capacity (Kw) | 20 |
| Oil reservoir capacity (gallon) | 200 |
| Machine size LxWxH (m/m) | 2480x1490x2945 |
| Net weight approx (kg) | 6500
7500 9500 |
HCBR-400T6S · Per-station specifications
| Clamping force (Ton) | 400 |
|---|---|
| Plate size (m/m) | 630×630 |
| Cylinder diameter (m/m) | 500 |
| Stroke (m/m) | 560 |
| Daylight (m/m) | 950 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 15 |
| Heater capacity (Kw) | 27 |
| Oil reservoir capacity (gallon) | 250 |
| Machine size LxWxH (m/m) | 2580x1500x3800 |
| Net weight approx (kg) | 6800
8000 10000 |
Start with the compound’s required molding pressure, total projected area under load at one station and cavity count. Then match mold footprint and height to the platen, daylight and stroke. Send the product photos or drawings you already have; you do not need to determine the tonnage before contacting Han Chang.
Equipment integration and production planning
Bring the pad dimensions, cavity layout and current hot-molding conditions into the selection discussion. Han Chang can help compare the five six-station models around the station load and installation space your molds need.
Separate per-station specifications from the complete installation’s supply scope when comparing quotations. Identify the press, tooling interfaces and site electrical requirements, then discuss the product mix and planned output so the equipment choice reflects actual production work.
Buyer questions
Why does the six-station layout suit one-operator tending?
Han Chang places the six workstations close together so one operator can move between charging, molding and part-removal tasks along a short route. Less walking between presses improves operating efficiency. Schedule the work around the curing and handling time of the products being made.
Which brake pads and friction compounds can it mold?
The machine is intended for hot molding disc brake pad friction blocks, including steel-backed products where the mold design accommodates them. Ceramic, semi-metallic and non-asbestos pad formulations can be considered when they use phenolic-bonded friction compounds suitable for hot pressing. Match heating and holding conditions to the actual material and tool.
How do I choose among the five six-station models?
HCBR-150T6S, HCBR-200T6S, HCBR-250T6S, HCBR-300T6S and HCBR-400T6S each have six workstations, rated at 150, 200, 250, 300 and 400 tons per station respectively. Select force from the required molding pressure, total projected area under load at one station and tooling loads. Then compare platen size, mold height, daylight and stroke.
Are the listed dimensions, weight and electrical ratings per station?
Yes. Every value in the specification tables applies to one station, including press force, platen size, machine dimensions, weight, motor rating and heater capacity. Han Chang supplies overall dimensions, weight and total electrical requirements separately for the complete six-station configuration.
How can the stations support a varied brake pad product mix?
Assign hot-molding work around the orders, pad designs and molds, with each product’s material and molded parts clearly organized. Closely spaced stations help the operator attend the work with less travel. Match the intended product combination to its tooling, molding conditions and handling times during model selection.
What should I compare when considering a multi-station press or an automatic line?
Choose Han Chang’s six-station arrangement for its close-access, one-operator workflow and practical support for multiple pad products. If the purchasing brief also calls for automatic weighing, transfer or loading and unloading, list those functions separately when comparing an automatic line’s supply scope. Start a quotation with the product photos, compound or tooling information available, and discuss output using parts per mold load and the full curing, cleaning and handling cycle.
Make one-operator, multi-station production work for your brake pads
Bring your pad designs and daily production needs to Han Chang. Send a product photo or mold drawing to compare six-station models and request a quotation for a brake pad hot press that keeps operator work close together.