
Double-Station Vacuum Compression Molding Machine
Han Chang manufactures double-station vacuum compression molding machines for rubber and silicone seals, gaskets and keypads. Each station operates independently; evacuation begins with pressing and venting after the mold and hood close.
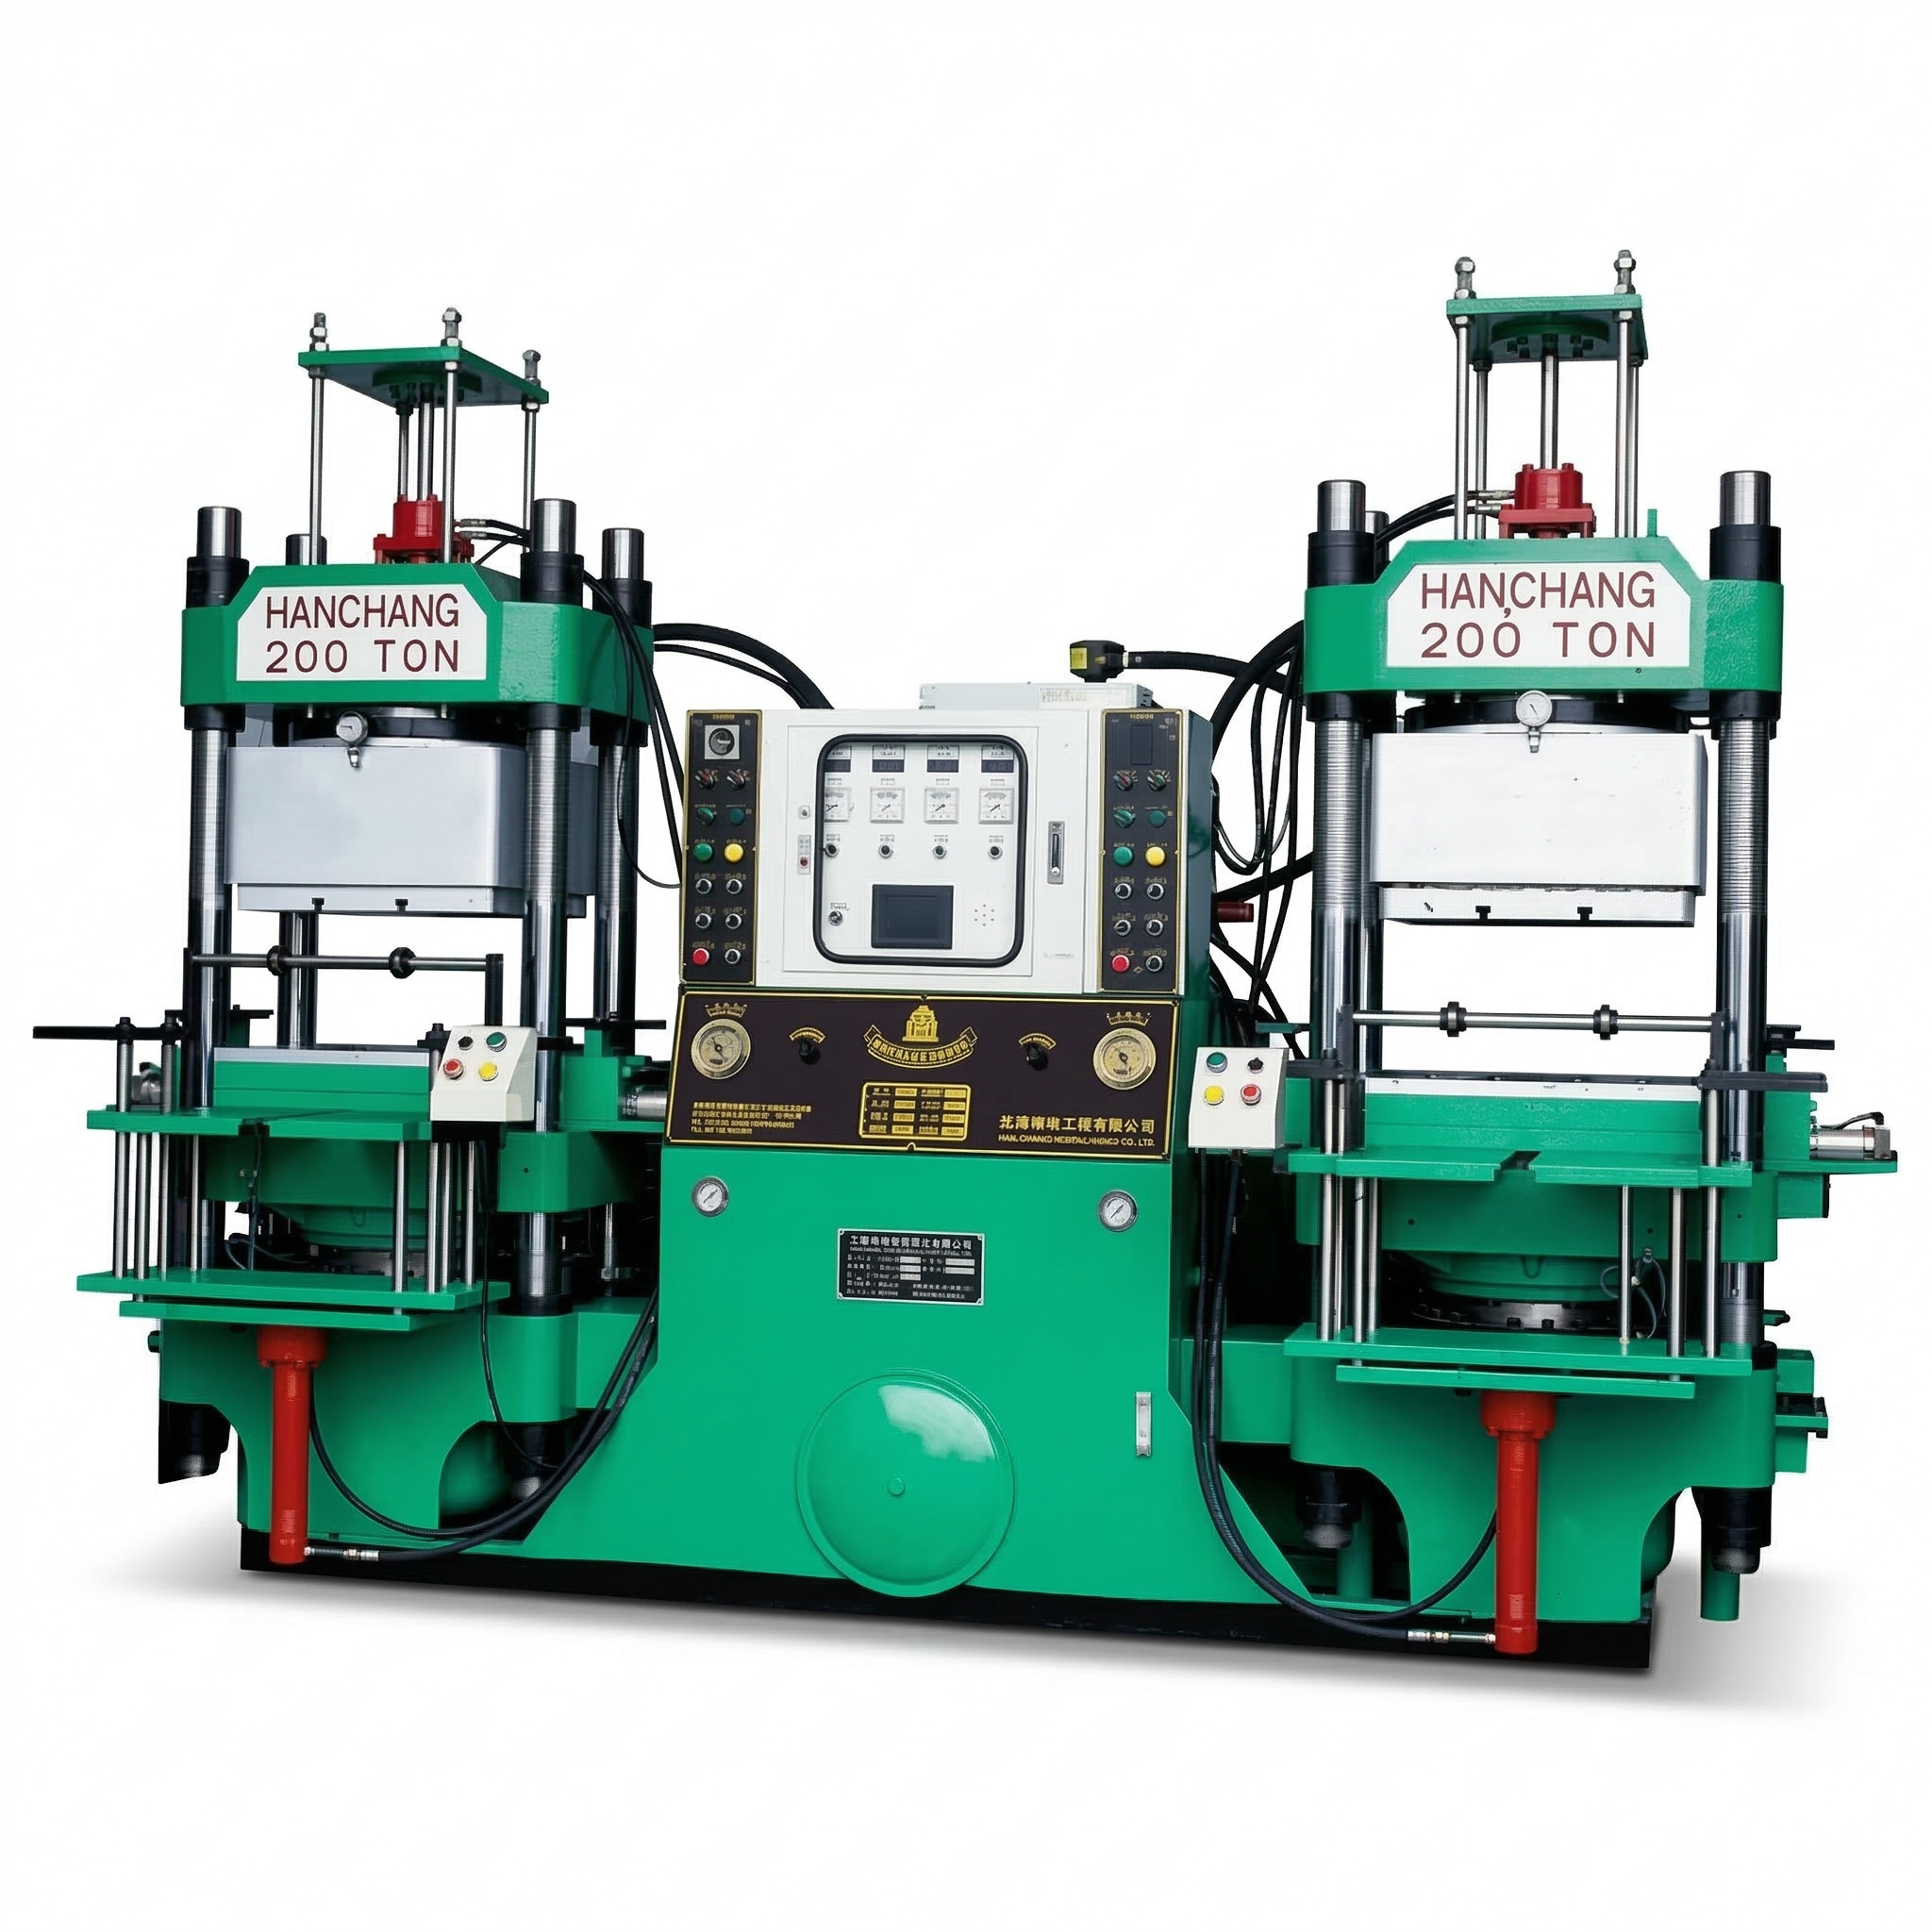
Machine advantages
Draw vented gases away from the mold
Vacuum evacuation works with mold degassing during pressing to carry released gases away from the molding area. This helps reduce the effect of trapped gas on sealing surfaces and part appearance.
Run one station when that is all you need
Independent left and right controls let you use either station on its own. Production does not depend on having both stations running together.
Heat and hydraulic force for both compounds
Heated platens supply heat and hydraulics apply molding force. Matching temperature, pressure and curing time to the rubber or silicone compound lets the same machine type serve different molded-product requirements.
Match press size to the complete mold
The 80–350 ton model range offers different molding forces and platen specifications. Select for the mold footprint and cavity layout, rather than the size of a single seal alone.
Vacuum compression molding and degassing
Open the mold and load compound
Open the mold and place the rubber or silicone compound inside.
Close the mold, then the vacuum hood
After loading, close the mold first, followed by the vacuum hood, ready for evacuation and pressing.
Evacuate while pressing and venting
Vacuum evacuation starts together with pressing and venting. The vacuum draws away released gases while heated platens provide heat for compression molding and curing.
Open and remove the part
Once molding is complete, open the mold and vacuum hood, then remove the finished part.
Rubber and silicone applications
Han Chang double-station vacuum compression presses mold rubber and solid-silicone products for machinery, electronics and consumer goods. Vacuum evacuation supports mold venting, while independently controlled stations provide flexible production scheduling.
O-rings, flange gaskets and equipment seals
Molded products include O-rings, flat sealing washers, flange gaskets, pump-cover seals and valve sealing pads. NBR is a common starting point for oil-resistant seals; EPDM is often considered for outdoor sealing applications.
Vacuum evacuation works with mold vents to remove gases around sealing faces and ring sections during compression molding.
Cable grommets, wiring boots and protective caps
Examples include panel grommets, wiring-harness boots, connector dust caps, rubber plugs and mechanism covers. These parts protect cables at panel openings and shield exposed connections or moving assemblies.
Vacuum assistance helps vent holes, grooves and thin edges. Mold splits and release paths are matched to undercuts or folded shapes.
Machine feet, rubber bumpers and vibration pads
Produce equipment feet, appliance anti-slip pads, impact bumpers, cushioning washers and resilient pads. Natural-rubber and SBR compounds are common choices where elasticity and wear performance guide material selection.
Heated platens and pressure holding cure the compound. Independent stations let production be scheduled around the molds and orders in use.
Silicone keypads and electronic enclosure seals
Solid-silicone products include remote-control keypads, industrial control-panel keymats, button dust membranes, connector seals and enclosure gaskets. Compound hardness helps define key feel, elastic return and sealing behavior.
Vacuum venting helps manage gas around thin keypad webs and sealing edges. Electrical contacts and printing belong to the wider keypad production process.
Suction cups, flexible diaphragms and bellows
Matched tooling can produce handling suction cups, pump or valve diaphragms, rubber bellows and silicone protective boots. Cup lips provide contact, diaphragms flex during operation, and bellows protect assemblies while allowing movement.
Vacuum evacuation supports venting around thin lips and changing wall sections; mold cores and parting lines provide the release path.
Silicone coasters, baking molds and wearable parts
Consumer-product examples include silicone coasters, heat-resistant mats, baking molds, soft grips and wristbands. Tool surfaces create the required contours and textures; compound, color and hardness determine the intended feel and use.
Independent stations support tool and batch scheduling, while vacuum assists surface venting. Food-contact products require suitable compounds and finished-part compliance testing.
Specifications and machine selection
Seven models, from HCAV-80D to HCAV-350D, cover the 80–350 ton range. Compare platen dimensions, stroke, maximum daylight, heater capacity and overall machine dimensions in the individual specification tables.
Spec / Type HCAV-80D
| Clamping force (Ton) | 80 |
|---|---|
| Plate size (m/m) | 439×419 |
| Cylinder diameter (m/m) | 236 |
| Stroke (m/m) | 320 |
| Daylight (m/m) | 500 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 5×2 |
| Heater capacity (Kw) | 7.6×2 |
| Oil reservoir capacity (gallon) | 150 |
| Machine size LxWxH (m/m) | 3140x1528x2185 |
| Net weight approx (kg) | 5400 |
Spec / Type HCAV-100D
| Clamping force (Ton) | 100 |
|---|---|
| Plate size (m/m) | 355×355
439×419 555×505 |
| Cylinder diameter (m/m) | 265 |
| Stroke (m/m) | 320 |
| Daylight (m/m) | 500 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 5×2 |
| Heater capacity (Kw) | 10.6×2 |
| Oil reservoir capacity (gallon) | 150 |
| Machine size LxWxH (m/m) | 3380x1793x2370 |
| Net weight approx (kg) | 7600 |
Spec / Type HCAV-150D
| Clamping force (Ton) | 150 |
|---|---|
| Plate size (m/m) | 439×419
555×505 614×574 |
| Cylinder diameter (m/m) | 300/315 |
| Stroke (m/m) | 320 |
| Daylight (m/m) | 500 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 7.5×2 |
| Heater capacity (Kw) | 10.6×2 |
| Oil reservoir capacity (gallon) | 150 |
| Machine size LxWxH (m/m) | 3750x1880x2370 |
| Net weight approx (kg) | 9000 |
Spec / Type HCAV-200D
| Clamping force (Ton) | 200 |
|---|---|
| Plate size (m/m) | 555×505
614×574 674×674 |
| Cylinder diameter (m/m) | 368 |
| Stroke (m/m) | 320 |
| Daylight (m/m) | 500 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 7.5×2 |
| Heater capacity (Kw) | 16.6×2 |
| Oil reservoir capacity (gallon) | 170 |
| Machine size LxWxH (m/m) | 3750x1860x2760 |
| Net weight approx (kg) | 12000 |
Spec / Type HCAV-250D
| Clamping force (Ton) | 250 |
|---|---|
| Plate size (m/m) | 614×574
674×674 785×710 |
| Cylinder diameter (m/m) | 400 |
| Stroke (m/m) | 320 |
| Daylight (m/m) | 500 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 7.5×2 |
| Heater capacity (Kw) | 16.6×2 |
| Oil reservoir capacity (gallon) | 170 |
| Machine size LxWxH (m/m) | 3750x1860x2760 |
| Net weight approx (kg) | 12500 |
Spec / Type HCAV-300D
| Clamping force (Ton) | 300 |
|---|---|
| Plate size (m/m) | 614×574
630×650 674×674 |
| Cylinder diameter (m/m) | 450 |
| Stroke (m/m) | 320 |
| Daylight (m/m) | 500 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 7.5×2 |
| Heater capacity (Kw) | 16.6×2 |
| Oil reservoir capacity (gallon) | 170 |
| Machine size LxWxH (m/m) | 3750x1965x2760 |
| Net weight approx (kg) | 13000 |
Spec / Type HCAV-350D
| Clamping force (Ton) | 350 |
|---|---|
| Plate size (m/m) | 700×700 |
| Cylinder diameter (m/m) | 460 |
| Stroke (m/m) | 320 |
| Daylight (m/m) | 500 |
| Pump pressure (kg/cm2) | 210 |
| Motor (HP) | 10×2 |
| Heater capacity (Kw) | 16.6×2 |
| Oil reservoir capacity (gallon) | 170 |
| Machine size LxWxH (m/m) | 3760x1965x2960 |
| Net weight approx (kg) | 14500 |
Match molding force and platen size first, then check mold thickness, opening clearance and room for part removal. If you do not know the required tonnage, start with your part drawing or existing mold dimensions and discuss model and heating requirements with Han Chang.
Tooling and equipment quotations
Start with a product photo, drawing or existing mold details. Han Chang can discuss molding force, platen size and opening clearance around the mold footprint, thickness, cavity count and space needed to remove parts.
Discuss heater capacity in relation to compound curing conditions and mold size and thickness. A quotation tied to the selected model and configuration makes equipment comparisons more useful.
A mold-tilting function can be customized around the tooling and operator access required for loading and demolding. Send a mold drawing or photo to discuss the arrangement.
Buyer questions
What rubber and silicone products can this double-station vacuum press mold?
Han Chang double-station vacuum compression presses can mold O-rings, equipment gaskets, cable grommets, protective caps, machine feet, bumpers, silicone keypads, enclosure seals, suction cups and flexible diaphragms, as well as silicone coasters, heat-resistant mats and baking molds. Suitable compounds and tooling define the product range. Vacuum evacuation supports mold venting, and independent stations provide flexible production scheduling.
What does vacuum add to a rubber compression molding press?
The vacuum hood provides evacuation alongside mold venting. On this machine, compound is loaded and the mold is closed first. The hood then closes, and evacuation begins together with pressing and venting, drawing away released gases while heat and hydraulic force support molding and curing.
How is this different from rubber injection molding?
This is a compression molding machine: compound is placed in an open mold before the mold and vacuum hood close. Rubber injection molding feeds compound into an already closed mold. The feeding method and tooling requirements are different.
Can the left or right station run on its own?
Yes. The left and right stations have their own independent control systems. Either station can be switched on for production without requiring both to run together.
Does a vacuum hood replace mold vents?
No. Mold vent paths allow gas to leave the cavities, and vacuum evacuation carries the released gas away. Vent grooves, parting surfaces and compound flow still matter because gas needs a clear route out of the mold.
How do I choose tonnage for O-rings or oil seals?
Select tonnage using cavity count, total projected area, the compound’s required molding pressure and mold construction—not just the dimensions of one part. Then match platen size, daylight and stroke to the tool. Han Chang can discuss a suitable model from your part and mold information.
Can I use an existing rubber compression mold?
Start with its dimensions and construction details. The mold footprint must suit the platens, while mold thickness and part-removal space must fit the available daylight and stroke. Space inside the vacuum hood, vent paths and heating requirements also determine the fit.
Should I choose a single- or double-station vacuum press?
Both machines process rubber and silicone with the same vacuum compression molding motions. The difference is station count. The double-station machine has independent left and right controls, so either or both can be used. Choose a single-station press when one molding station suits the production plan; material alone does not decide the layout.
What information is needed for a machine quotation?
Send a product photo or drawing, the rubber or silicone compound and your planned production requirements. If tooling already exists, add the mold dimensions, thickness and cavity count. Han Chang can then discuss tonnage, platen size and heating requirements for a corresponding quotation; you do not need to specify the complete machine first.
Choose a double-station vacuum press for rubber and silicone
Send a product photo, drawing or mold details with your compound and production requirements. Han Chang can discuss molding force, platen size and heating configuration, then quote the corresponding machine.





